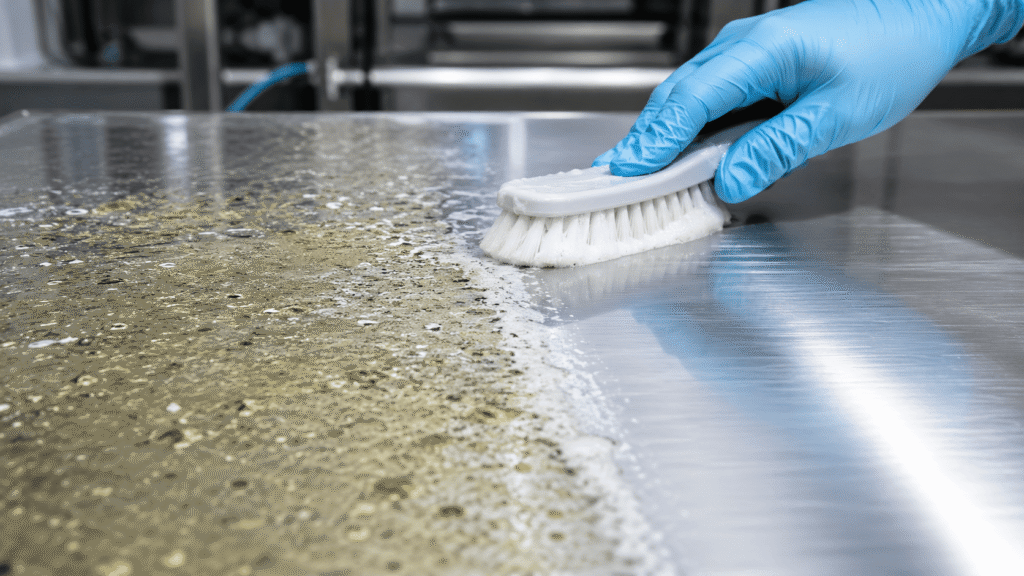
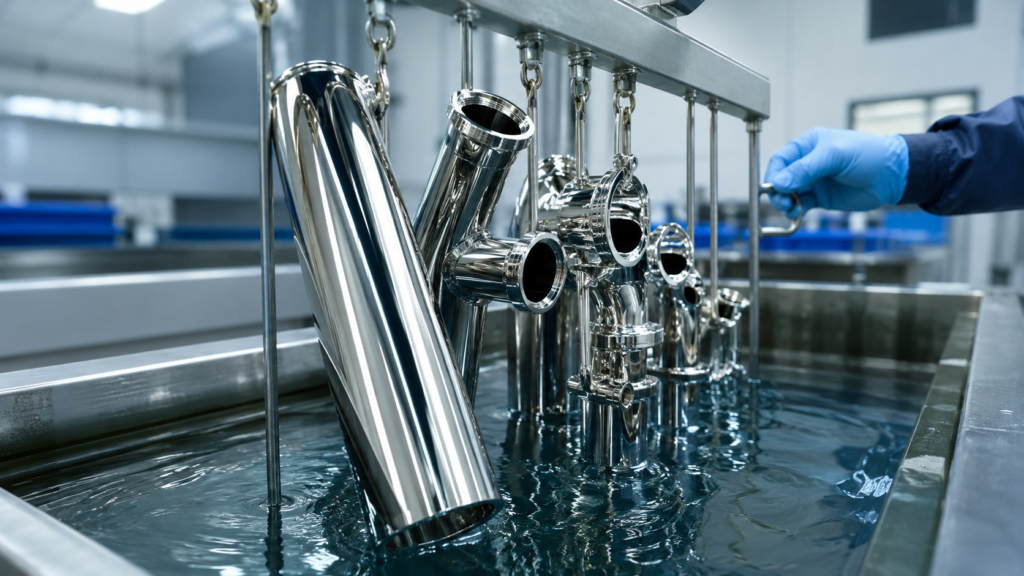
Pickling and passivation solve two different problems. Pickling removes heat tint, weld scale and the chromium-depleted layer left by welding, using acids that dissolve a thin layer of the surface. Passivation removes free iron so the stainless steel can form its protective chromium oxide layer. After welding or fabrication, stainless steel is usually pickled first and passivated second. A system that only needs free iron removed can go straight to passivation.
Stainless steel systems are widely used across industries such as pharmaceutical manufacturing, biotechnology production, food processing, and chemical processing. Maintaining corrosion resistance and system cleanliness is essential for ensuring operational reliability and regulatory compliance. Two processes commonly used to treat stainless steel surfaces are pickling and passivation. While both processes remove contaminants and improve metal performance, they serve different purposes and are applied in different situations. Knowing which one your system needs, or whether it needs both, decides the scope of the job.
What Is Stainless Steel Pickling?
Pickling is a chemical treatment process used to remove heavy surface contaminants from stainless steel. These contaminants typically include:
- weld scale
- heat tint
- oxidation
- surface discoloration
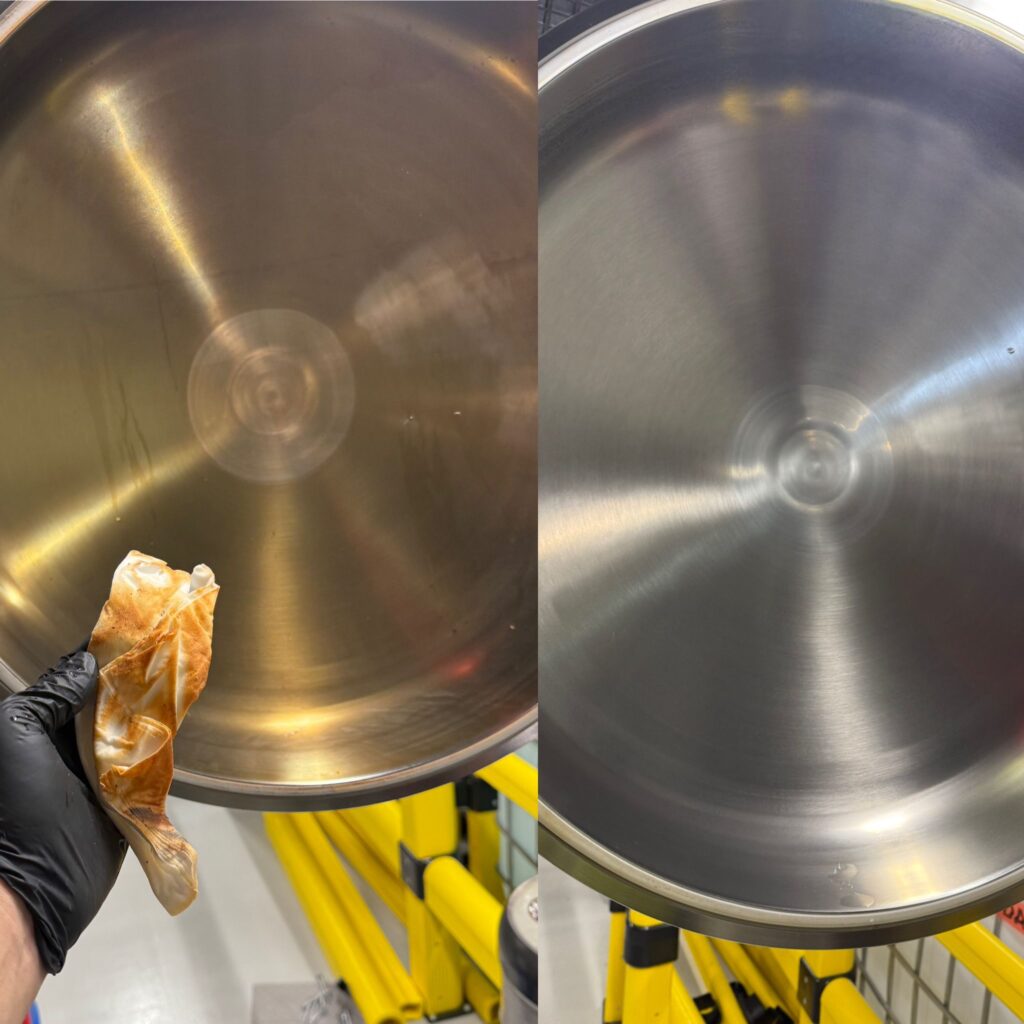
When stainless steel is welded or exposed to high heat, a colored oxide layer forms on the surface. Beneath it is a zone where the chromium content has been depleted. Chromium is what makes stainless steel corrosion-resistant, so that zone is where corrosion starts. To restore the surface, both the oxide and the chromium-depleted layer have to come off.
Standard pickling solutions are a mixture of nitric acid (HNO₃) and hydrofluoric acid (HF). Together they dissolve the oxide layer and the depleted metal underneath, exposing a fresh, fully alloyed stainless steel surface. They also remove ferrous and ferric oxides that can contribute to corrosion. For applications where environmental, safety or material compatibility is a concern, alternative formulations are available, including less aggressive acid blends and proprietary chemical treatments.
Grinding and abrasive blasting can also remove heat tint, but they can embed abrasives or iron particles in the surface, which leads to localized corrosion. They’re also impractical on complex geometries and internal surfaces such as piping. That’s why chemical pickling is the preferred method for welded systems.
What Is Stainless Steel Passivation?
Passivation is a chemical process that removes free iron contamination from the surface of stainless steel. Once the iron particles are removed, the metal forms a thin protective chromium oxide layer that protects the stainless steel from corrosion. Facilities often rely on professional stainless steel passivation services to treat stainless steel piping systems, tanks, and process equipment used in high-purity manufacturing environments.
Pickling vs Passivation: Key Differences
| Process |
Purpose |
Typical Application |
| Pickling |
Removes heavy scale, heat tint, and oxidation |
Post-welding or fabrication treatment |
| Passivation |
Removes iron contamination and restores corrosion resistance |
Final treatment for stainless steel systems |
Both processes can play a role in stainless steel surface treatment, but passivation is typically the final step required to restore corrosion resistance.
Pickling and Passivation in Sequence
On a newly welded or fabricated system, the two treatments usually run back to back. Pickling removes the heat tint, scale and chromium-depleted layer. Passivation then removes any remaining free iron and lets the chromium oxide layer form across the fresh surface.
Both are covered by ASTM standards. ASTM A380 covers cleaning, descaling, pickling and passivation of stainless steel equipment. ASTM A967 covers chemical passivation and the tests that verify it. BCS works to ASTM A380/A380-25 for cleaning and descaling and ASTM A967/A967M-25 for passivation, with Ferroxyl testing, a validation report and a Certificate of Compliance on every project. Our ASTM A967 vs. A380 guide explains how the two standards divide the work.
Why Passivation Is Critical for High-Purity Industries
Industries such as pharmaceutical manufacturing, biotechnology, and food processing require stainless steel systems that maintain strict cleanliness and corrosion resistance standards. Professional passivation services in North America help ensure that stainless steel piping and process systems meet industry expectations for durability and performance. If your team is also evaluating timing, this guide on when stainless steel piping should be passivated can help clarify when passivation is most important.
Pickling and Passivation Services at BCS BioClean
BCS BioClean has provided pickling and passivation services for over 30 years on stainless steel tanks and vessels, welded piping and tubing systems, heat exchangers, clean steam and gas distribution lines, RO, DI and WFI water systems, and product contact surfaces and components.
Our Oakville shop runs numerous acid and degreasing tanks, two of them 45 feet long, a fully MOE certified and inspected clean air scrubber system, ovens for baking and curing, and a 3-tonne overhead crane. For passivation on its own, see our passivation services, which use our BIOPASS® line of biodegradable, non-flammable, acid-based chemicals.
Frequently Asked Questions
What’s the difference between pickling and passivation?
Pickling removes heat tint, weld scale and the chromium-depleted layer from stainless steel by dissolving a thin layer of the surface. Passivation removes free iron so a protective chromium oxide layer can form. Pickling restores the surface; passivation protects it.
Do you need to pickle stainless steel before passivating?
Only if there’s heat tint, scale or oxide to remove, which is usually the case after welding or fabrication. A system without that damage can be passivated directly.
What acid is used to pickle stainless steel?
Standard pickling solutions are a mixture of nitric acid and hydrofluoric acid. Less aggressive acid blends and proprietary treatments are available where environmental, safety or material compatibility is a concern.
Can grinding or blasting replace pickling?
They can remove heat tint, but they can embed abrasives or iron particles in the surface and cause localized corrosion. They also can’t reach internal surfaces of piping. Chemical pickling avoids both problems.
Which standards cover pickling and passivation?
ASTM A380 covers cleaning, descaling, pickling and passivation of stainless steel. ASTM A967 covers chemical passivation and its verification. In pharmaceutical and biotech systems, ASME BPE 2026 also applies.
Does BCS BioClean offer pickling and passivation services?
Yes. We pickle and passivate tanks, vessels, welded piping and tubing, heat exchangers, clean steam and gas lines, water systems and product contact components, with shop tanks up to 45 feet long.